
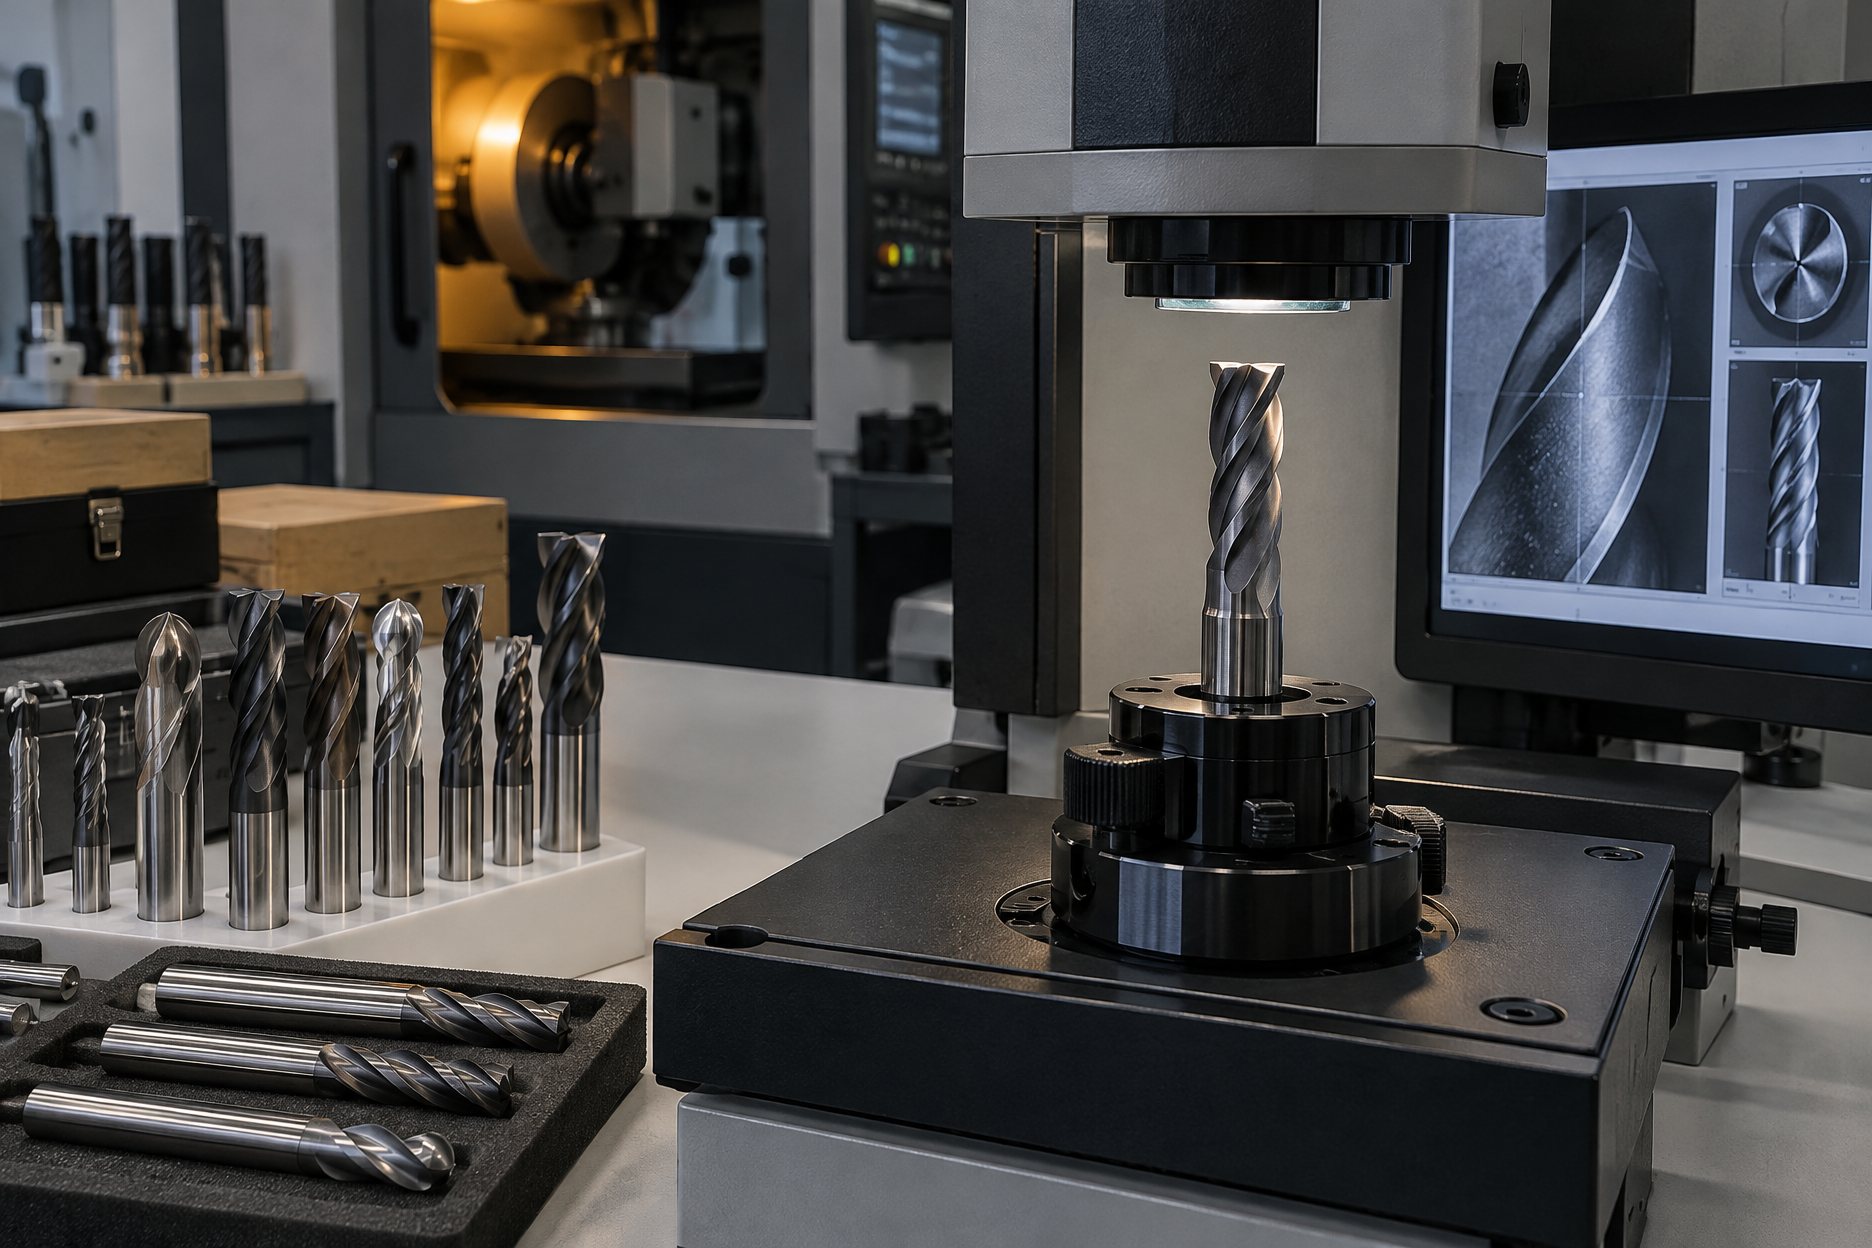
The standard is the sample, not a catalog photo
Every credible check in this trade compares the tool against something fixed. On desk programs the fixed points are two: the approved sample you signed off, and the program spec sheet that names every geometry line, the substrate, the coating, the marking and the packing. A bulk batch is checked against those - never against a catalog photo, never against a verbal description, and never against a different program's numbers. That is the whole philosophy, and everything below is its working details: what gets measured at which point, what the results feed, and which papers travel with the shipment so the checks mean something at your receiving dock, not just at the factory bench.
It also runs in the right order. Inspection sits after coating and marking, before boxing - the last gate, so a failed check stops boxes rather than starting them. Where a program's quantities justify it, checks also happen earlier in the chain: blank substrate confirmed in writing at the start, first-article checks off the grinder before the batch proceeds. The plan per program is written before sampling, not improvised at the end.
The inspection points
| Check | What is measured | Where it sits |
|---|---|---|
| Optical geometry | Diameter, flute geometry, corner and profile against the spec sheet | After coating and marking, before boxing |
| Runout | Total indicator runout at the cutting edge | Same gate, on the inspection bench |
| Coating appearance | Even coverage, color consistent with the coating family, adhesion spot checks | After the coating batch |
| Marking | Logo, geometry code and part number against the approved proof | After laser marking |
| Packing | Box counts, geometry labels, carton condition | At boxing, before freight |
Two of these deserve more words. Optical measurement is what makes geometry claims falsifiable: diameter, flute profile and corner shape are projected and measured, not eyeballed, so a line on the spec sheet is either within its stated tolerance or it is not - and the result can be reported to you per batch. Runout is measured at the cutting edge because that is where it costs you: total indicator runout at the edge feeds directly into how the tool wears and how your finish comes out, which is why the trade checks it rather than assuming it. The background is in the runout note and the buyer-facing checklist in the inspection checklist.
Runout, without invented numbers
Some supplier pages quote a universal runout figure for every tool they sell. We do not, because a single number is either so loose it means nothing or so tight it will not hold across every geometry in a program. What the desk does instead: acceptance is set per program, confirmed on the spec sheet before sampling, and the check is run against that line. A finishing program and a roughing program can carry different acceptance criteria and both be honest - the sheet is what keeps them that way. If your customers specify a runout expectation, write it into the program before the sample is cut - the sheet is the least costly place to hold a number.
Coating, marking and packing checks
The coating check is deliberately practical: even coverage across the flutes, color consistent with the named coating family, and adhesion spot checks on the batch. It is a screen for process problems - a contaminated fixture, a misloaded batch - rather than a laboratory report, and it is sized to the program. The marking check compares what the laser put on the shank against the proof you approved: content, position, legibility. The packing check is the least glamorous and the one your customers touch first - box counts correct, geometry labels matching the contents, cartons dry and intact. Programs fail in shipping more often than they fail in grinding, which is why the desk watches the carton as seriously as the flute.
Papers that travel with the shipment
Checks that produce no paperwork protect nobody downstream. Each program ships with a certificate of conformance for the shipment, and material certificates for the substrate - the mill cert for the carbide or HSS - are collected per program. The papers come from the producing factory, are provided in writing, and are part of the program sheet, so your receiving team, your auditor or your customer's quality department can trace the batch. What US import paperwork adds to this - origin marking, classification - is on the compliance page, and it is a customs broker question rather than a factory one.
Who checks, and who answers
The producing factory inspects as part of its chain; the desk's role is to make sure the checks are the ones you agreed to, run against the sheet you approved, with results you actually receive. Disputes, when they happen, resolve against the same two fixed points - sample and sheet - which is why the desk insists on both being settled before bulk. This division is also why the desk never describes the factories as its own: an independent producer with a written program and a named inspector is a stronger quality setup than a vague claim of in-house control. The desk's position is described in about Millcrown.
Adding your own checks
Programs can carry your inspection requirements: an incoming check you want replicated, a dimension your customers audit, a sample retention you want kept per batch. Write them into the program before sampling and they become part of the plan the factory prices and runs against - added after production, they become arguments. If you are building an acceptance plan now, send the checks you need with the quote form, and the desk will fold them into the sheet with reference timelines from the MOQ and lead time page. Substrate questions that sit behind the geometry are in the carbide grades note.